Head Office
117, Grand Trunk Road, Salkia Howrah-700013, Kolkata, India
 Hitesh PathakThu, Aug 28, 2025
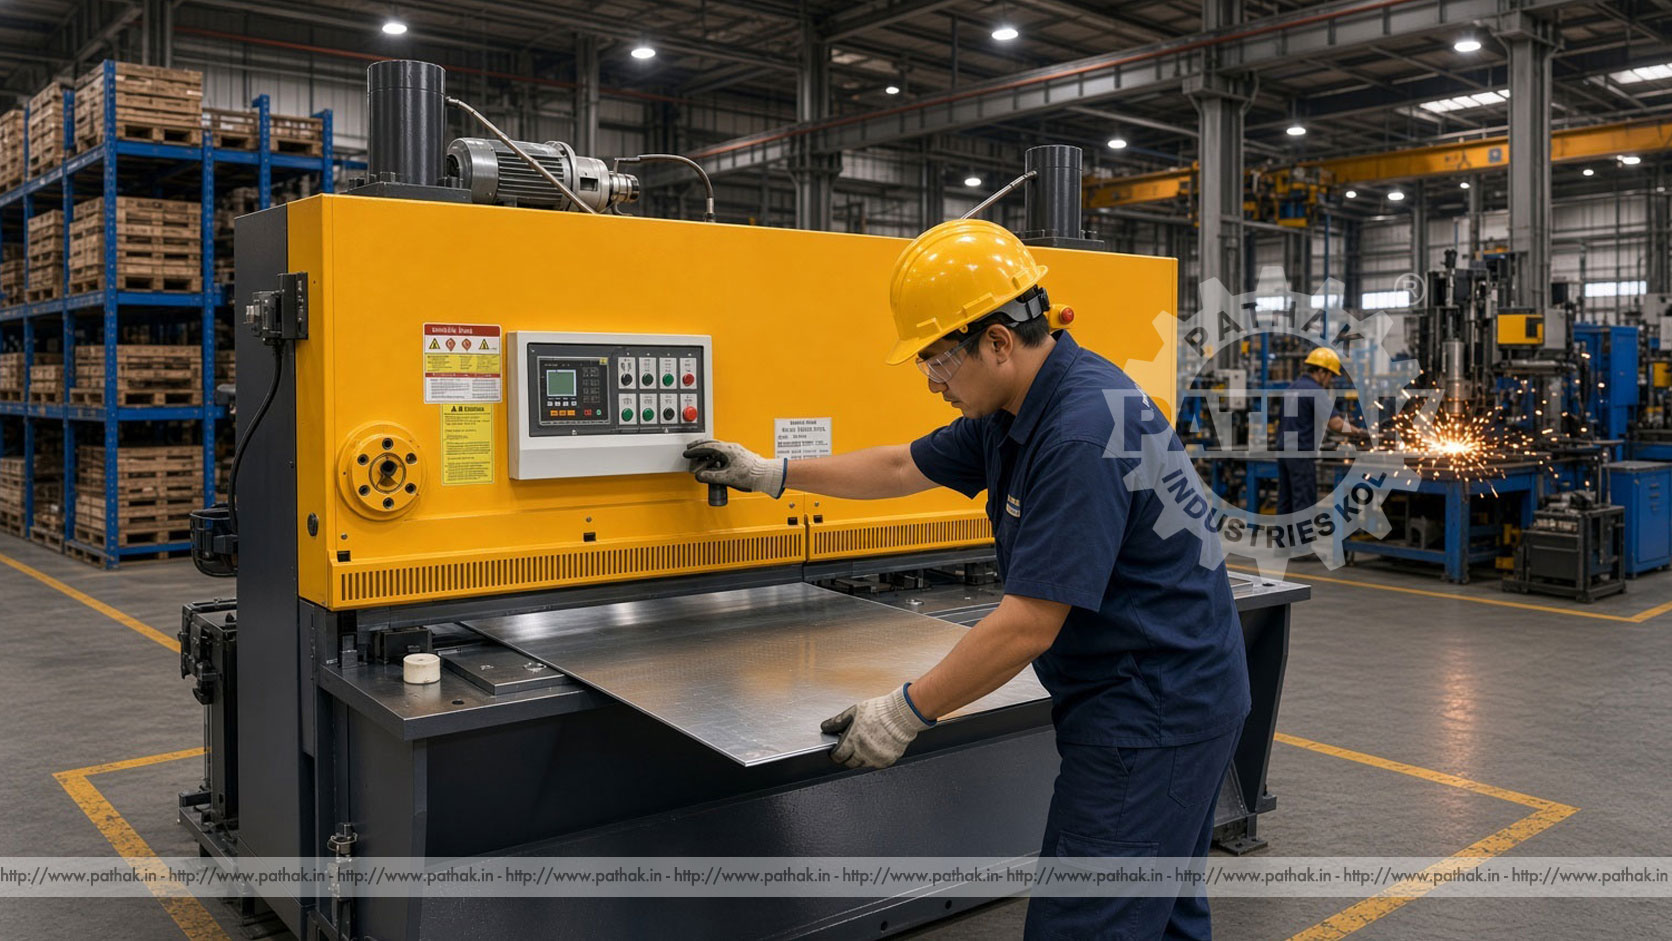
Turning a flat sheet or plate into a useful enclosure, bracket, channel, panel, or structural profile requires more than applying force along a line. The bend must occur in the correct position, at the required angle, and without damaging the material or tooling. A CNC Press Brake Machine combines a powered ram, matched punch-and-die tooling, work positioning, and programmable motion to make this controlled forming process practical for individual parts and repeat production.
The Pathak Industries product range includes CNPB models with published bending capacities from 50 to 200 tons and bending lengths from 2050 to 4050 mm. Those figures describe machine ratings, not a universal promise that every material can be bent across the full length. Material grade, thickness, bend length, die opening, tooling condition, grain direction, bend method, and required radius all affect the force needed. Correct selection therefore starts with the actual component rather than tonnage alone.
A press brake forms straight bends by driving a punch toward a matching die while the workpiece is positioned between them. As the sheet enters the die opening, it yields along the intended bend line. The tooling profile and programmed ram movement determine the basic geometry, while material behaviour influences the final angle after pressure is released.
CNC control adds programmable positioning and cycle management. Depending on the supplied configuration, the operator can prepare values for ram travel and work positioning, recall established jobs, and reproduce a bending sequence more consistently than with repeated manual adjustment. CNC does not remove the need for skilled setup: tooling choice, tonnage checks, bend allowance, safe handling, and first-part inspection remain essential.
The process begins with a drawing that defines material, thickness, dimensions, bend angles, inside radii, and tolerances. A flat pattern is cut to size, deburred, identified, and brought to the machine. Suitable punch and die sections are selected, inspected, installed, aligned, and secured. The operator then prepares the program and sets the work-positioning system for each bend.
During the cycle, the sheet is located against the programmed reference, the ram approaches, and the punch forms the material into the die. The ram then returns so the component can be repositioned for its next bend. A trial part is measured before the job is released for production. Corrections may be required because real sheet varies in thickness, strength, surface condition, and springback.
The published range begins with model CNPB-0520, rated at 50 tons with a 2050 mm bending length. CNPB-0825 is rated at 80 tons across 2550 mm. The 100-ton options include CNPB-1030 at 3050 mm and CNPB-1040 at 4050 mm. These choices allow a buyer to distinguish between capacity and working length instead of assuming that a higher figure is automatically the best fit.
The range continues with 135-ton CNPB-1330 and CNPB-1340 models, offering 3050 and 4050 mm bending lengths respectively. CNPB-1630 and CNPB-1640 provide the same length choices at a stated 165-ton capacity. At the upper end, CNPB-2030 and CNPB-2040 are rated at 200 tons with bending lengths of 3050 and 4050 mm. A bending calculation is still required for every proposed material, length, thickness, die opening, and method.
Distance between uprights affects the width that can pass within the frame. Published values range from 1640 mm on CNPB-0520 to 3150 mm on the 4050 mm models. This dimension must be considered separately from overall bending length, particularly when a component must enter between the side frames or when an off-centre setup is being evaluated.
All listed models have a 900 mm table height. The published throat depth is 300 mm on CNPB-0520 and 400 mm on the remaining models. The 50- through 165-ton machines list a 200 mm ram stroke, while the 200-ton models list 250 mm. Distance between table and ram is stated as 380 mm for the first two models, 400 mm across the 100- to 165-ton group, and 450 mm for the 200-ton machines. Tool height and workpiece geometry must fit within these available spaces.
A press brake cycle includes more than the actual forming movement. The ram approaches the job, performs the working stroke, and returns. The listed working speed is 10 mm/s across the range. Published approach speed varies by capacity: 150 mm/s for CNPB-0520 and CNPB-0825, 130 mm/s for the 100-ton models, 120 mm/s for the 135- and 165-ton models, and 100 mm/s for the 200-ton pair.
Return speed is listed at 110 mm/s from the 50- through 165-ton models and 100 mm/s for the 200-ton machines. These figures help describe cycle movement, but real production output also depends on loading, alignment, number of bends, part turning, inspection, unloading, and operator safety. A faster approach alone does not define parts per hour.
Tooling has a direct effect on bend radius, required force, surface condition, and achievable geometry. The punch must suit the desired profile and clear surrounding flanges. The die opening must be appropriate for the material and bending method. Tool sections must also be rated for the applied load; an otherwise capable machine cannot safely compensate for overloaded tooling.
Before installation, clean the tool seating surfaces and inspect the punch and die for damage. Segmented tools should be arranged and secured correctly. Alignment must be checked across the working length, especially when several sections form one bend. Tool identification and organised storage reduce setup errors and protect precision surfaces from accidental impact.
Sheet metal stretches on the outside of a bend and compresses on the inside. The neutral region shifts as the bend forms, so the flat blank cannot be calculated simply by adding finished flange dimensions. Bend allowance and bend deduction are used to create the correct flat pattern. These values depend on thickness, inside radius, material, and the forming method.
Springback occurs when elastic recovery opens the bend after the forming force is removed. Different grades and batches can behave differently even at the same nominal thickness. CNC programming supports controlled corrections, but first-part measurement remains important. For repeat jobs, recording the successful program, tooling, material specification, grain direction, and measured correction helps reduce future setup time.
CNC press brakes are used in sheet metal workshops that manufacture electrical enclosures, machinery guards, cabinets, trays, channels, brackets, covers, panels, duct components, equipment frames, and fabricated assemblies. They also support contract fabrication where part sizes and batches change regularly. Programmable positioning is valuable when a component has several bends or when a proven job returns periodically.
The machine can serve production units, equipment manufacturers, maintenance workshops, infrastructure suppliers, and fabrication businesses. Suitability always depends on the component. A long light-gauge panel presents different handling and straightness challenges from a short thick bracket, even if both fit within the nominal machine length.
A multi-bend component needs a sequence that avoids collisions between the formed flanges, punch, die, ram, and machine frame. Operators should consider whether an early bend will prevent the sheet from being positioned for a later one. Part orientation and safe support also matter because the centre of gravity changes as the shape develops.
Where possible, establish a setup sheet containing the program reference, tooling, station positions, bend sequence, material, inspection points, and approved corrections. Marking the correct face and bend direction helps prevent reversed parts. The first completed component should be checked against the drawing before the remainder of the batch is formed.
Begin with a representative list of parts. Record maximum bend length, material grades, thicknesses, flange sizes, desired radii, annual quantities, and the number of bends per component. Use recognised bending calculations to determine required force for each case, including a suitable margin. Never assume that total machine tonnage can be concentrated at any point without checking permissible load distribution.
Next compare bending length, distance between uprights, throat depth, ram stroke, open height, and tooling space. Consider the overall machine dimensions and weights published for installation planning. The listed weights range from 5000 kg for CNPB-0520 to 14,000 kg for CNPB-2040. Foundation, access, lifting, unloading, and final positioning should be planned before delivery.
Motor power is published from 6 kW on CNPB-0520 through 20 kW on the 200-ton models, while oil tank capacities range from 180 to 400 litres. Electrical supply, hydraulic service needs, ambient conditions, and maintenance access must all be confirmed for the selected machine. Pathak Industries can review workpiece details against the published range before a final configuration is chosen.
The closing area between punch and die presents a serious crushing hazard. Operators must be trained in the supplied controls, safeguarding, tooling procedures, emergency functions, and safe setup method. Guards and protective devices should never be bypassed. Tool changes, cleaning, adjustment, and maintenance require isolation according to the machine instructions and site procedure.
Large sheets require a handling plan. Unsupported material can drop, swing, or rise during bending, placing the operator and nearby workers at risk. Suitable supports or lifting assistance may be necessary. Hands must remain outside hazardous zones, and loose clothing should be controlled. The floor should be kept clear of offcuts, oil, and obstacles.
Consistent forming depends on a machine that remains clean, lubricated, aligned, and hydraulically sound. Daily checks should cover visible leaks, tooling security, guards, controls, abnormal sounds, and the working area. Tool surfaces and seating locations should be kept free of scale and debris. Damaged tooling should be removed from service rather than compensated for through programming.
Hydraulic oil condition, filters, seals, guides, fasteners, electrical cabinets, sensors, and positioning components require attention at the intervals specified by the manufacturer. Accuracy checks should use suitable measuring equipment and a documented method. Maintenance and calibration records help distinguish machine drift from changes caused by material or tooling.
It forms straight bends in sheet and plate by moving a punch into a matched die. CNC control programs machine motion and positioning to support repeatable bend sequences.
The published CNPB range covers rated bending capacities from 50 to 200 tons, with bending lengths from 2050 to 4050 mm. The required model must be confirmed through a calculation for the actual work.
No. Required force changes with material strength, thickness, bend length, tooling, die opening, radius, and bending method. Machine and tooling load limits must both be observed.
It provides a repeatable reference for locating the bend line. Accurate positioning reduces dimensional variation, although part preparation, handling, tooling, and inspection still influence the result.
Selection depends on material, thickness, desired radius, bending method, available flange, and tooling capacity. Use the tooling provider’s data and the approved bending calculation for the job.
The material recovers elastically after the load is released, which can open the angle. The amount varies by material and geometry and is addressed through controlled setup and measured correction.
Provide material grades, thickness range, maximum bend length, component drawings, desired radii, production quantities, electrical supply, tooling needs, and available installation space.
Follow scheduled checks for hydraulics, lubrication, guides, tooling seats, fasteners, electrical systems, safeguards, and positioning accuracy. Isolate the machine before service and use qualified personnel.
A CNC press brake delivers its best value when machine capacity, working dimensions, tooling, programs, and material handling are planned as one system. The Pathak CNPB range provides multiple combinations of tonnage and bending length for different fabrication requirements. Careful part analysis prevents both under-selection and unnecessary investment in capacity that the workshop will not use.
Review the complete model table on the CNC Press Brake Machine product page, then share representative drawings and production details for application assessment. Final capacity, tooling, configuration, foundation, and utilities should be confirmed before ordering.